

Zamak is a family of zinc-based casting alloys used widely for detailed, repeat-production components. The name comes from the German names for zinc, aluminum, magnesium and copper, the elements that define the conventional alloy family. In practice, the word “Zamak” usually refers to zinc die-casting alloys such as Zamak 2, 3, 5 and 7 rather than to a single material grade.
Zamak is a strong candidate when a product needs complex geometry, good surface finish, consistent dimensions and efficient high-volume production. It is not automatically the right answer for every part: density, service temperature, creep resistance, corrosion environment, wall section and finishing requirements must all be evaluated alongside cost.
What Zamak is made of
Zinc is the base metal in conventional Zamak alloys. Aluminum supplies much of the alloy family’s strength and castability; magnesium helps control intergranular corrosion behavior and supports dimensional stability; copper can raise strength and hardness but may also change ductility and long-term behavior. Exact composition limits vary by grade and applicable material standard, so a drawing should call out the required alloy designation rather than merely saying “zinc.”
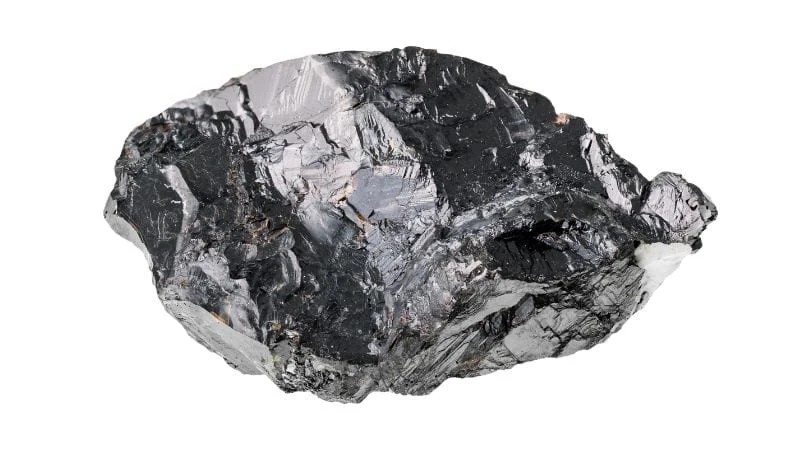
Conventional Zamak alloys are distinct from the higher-aluminum ZA alloy family. They can share a zinc base, but their composition, properties and process fit are not interchangeable. Treat Zamak 3, ZA-8 and ZA-27 as different engineering choices, not informal substitutes.
Zamak 2 vs 3 vs 5 vs 7
Zamak 3 is widely used because it balances castability, dimensional stability and finishing performance. It is a sensible starting point, not a default that eliminates engineering review. Select the grade from the product’s loads, geometry, operating temperature, life expectations, surface finish and post-casting operations.
| Grade | Selection focus | Typical fit | Important trade-off |
|---|---|---|---|
| Zamak 2 | Higher strength and hardness within the conventional family | Wear-oriented and structural hardware where the design supports the alloy | Less ductile than Zamak 3; validate creep and secondary-forming needs |
| Zamak 3 | Balanced, general-purpose zinc die-casting alloy | Hardware, housings, handles, consumer components and many plated parts | Do not assume it is the best grade when creep, wear or ultra-thin detail controls the design |
| Zamak 5 | Added copper for higher strength, hardness and improved creep resistance relative to Zamak 3 | Mechanical components and parts where extra tensile performance is needed | The property increase comes with lower ductility than Zamak 3 |
| Zamak 7 | Improved fluidity, ductility and surface finish characteristics | Fine-detail, thin-wall or finish-critical castings | Specify the quality and impurity limits required; do not select on grade name alone |
Why Zamak works well for die casting
Most Zamak components are made by high-pressure hot-chamber die casting. The process can fill detailed cavities rapidly, then eject the casting in a short, repeatable cycle. The relatively low processing temperature of conventional zinc alloys supports long die life compared with higher-temperature casting alloys, while the alloy’s flow behavior can reproduce fine features and clean surface texture.
Die casting is most valuable when it replaces repeated machining or assembly work with a near-net-shape part. Ribs, bosses, mounting features, logos, detailed external forms and certain internal features can be designed into the casting. Critical threads, precision bores, bearing seats, sealing surfaces and highly cosmetic areas may still need secondary operations or specified process controls.
For an OEM tooling program, see Moldiecasting Zamak die casting molds. The page outlines DFM, gating, runners, venting, ejection, CNC mold manufacture and tryout support for production tooling.
Key properties and limits to consider
Zamak can offer useful strength, hardness, impact performance and machinability for small-to-medium precision components. It also accepts a range of finishing routes, including plating, painting and coating, when the substrate preparation and finish specification are compatible. This makes it common in functional hardware where appearance matters as much as fit.
The alloy’s limitations are just as important. Zinc alloys are denser than aluminum and magnesium, so Zamak may not suit weight-sensitive designs. Elevated temperature can reduce load-carrying capability over time through creep; the allowable temperature and stress depend on the grade, part geometry and life target. Corrosion performance should be assessed for the actual atmosphere, moisture, chemicals, galvanic couples and chosen finish rather than assumed from a general statement about zinc.
For pressure-tight components, state the pressure, medium, temperature, test method and leak-acceptance criteria. High-pressure die casting can create entrapped-gas or shrinkage-related porosity if part design and process control are not appropriate; “die cast” alone is not a pressure-tightness guarantee.
Design guidelines for Zamak die casting
- Keep walls as uniform as the function allows. Sudden thick sections cool differently, which can increase shrinkage, porosity and distortion risk.
- Add draft in the direction of die opening. Draft supports ejection and protects both surface quality and tool life.
- Use radii instead of sharp corners. Fillets help metal flow, reduce stress concentration and make the cavity easier to manufacture.
- Define the parting line and cosmetic surfaces early. Gate vestige, ejector marks and parting-line evidence need an agreed location when appearance is important.
- Separate as-cast and machined tolerances. Reserve machining for features that truly need it, and include practical machining stock where appropriate.
Moldiecasting’s die casting mold design and engineering service reviews wall thickness, corners, draft, gating, runners, cooling and ejection before steel is cut.
Common Zamak applications
Zamak is often chosen for locks, handles, furniture hardware, bathroom fittings, lighting components, electronics housings, automotive trim and mechanisms, small gears, consumer-product features and decorative components. These applications benefit from the combination of detail, repeatability, finishability and near-net-shape production.
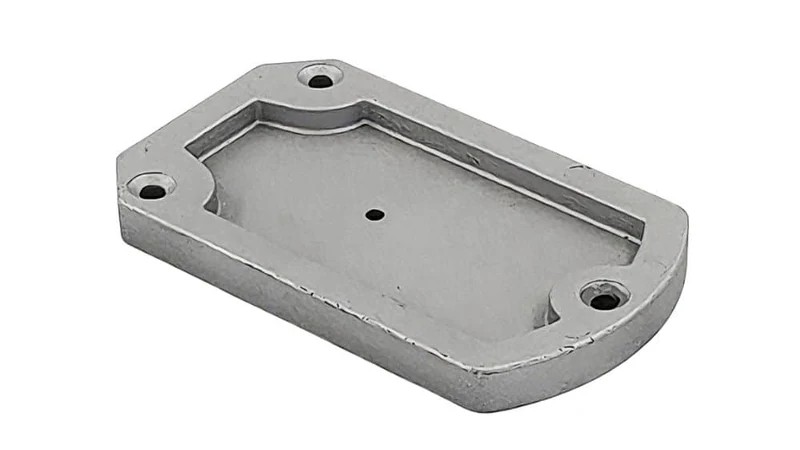
The application name does not select the alloy by itself. A door handle, for example, may have cosmetic plating and a low mechanical load; a gear may have a wear and creep requirement; an electrical enclosure may prioritize dimensional control and grounding strategy. Define the failure modes and validation conditions before choosing the grade and process.
For lock and hardware tooling applications, browse Moldiecasting zinc die casting molds and share the CAD model and service requirements for a DFM discussion.
Zamak vs aluminum, magnesium and brass
If Zamak is not the best material for the function, compare aluminum die casting molds or magnesium die casting molds with your engineering requirements.
| Material route | Consider it when | Evaluate carefully when |
|---|---|---|
| Zamak / zinc alloy | Fine detail, compact components, quality surface finish and high-volume repeatability matter | The product is weight-sensitive, operates at elevated temperature or has demanding creep/pressure-tightness requirements |
| Aluminum die casting | A lighter housing, thermal function or larger structural component is needed | Very fine detail and low-temperature hot-chamber productivity are the main value drivers |
| Magnesium die casting | Mass reduction dominates the design brief | Corrosion protection, stiffness, application environment and process fit need review |
| Brass or copper-base alloy | Wear, corrosion resistance or a specific electrical/appearance property justifies it | Higher density, higher process temperature and tooling demands make the total program cost less favorable |
How to prepare a useful Zamak tooling inquiry
A complete quote request reduces iteration and produces a more meaningful tooling proposal. Provide the 3D model and 2D drawing, desired Zamak grade or functional requirements, annual and lifetime volume, press tonnage if known, target part weight, critical tolerances, cosmetic class, finish, secondary operations, inspection plan, performance tests and project timing. Flag pressure sealing, safety-related loads and regulated material requirements early.
Start Your Zamak Tooling Project with Moldiecasting
Moldiecasting can review your part geometry, alloy preference, annual volume and quality requirements before tooling is released. A focused DFM discussion helps align the die design, gating, venting, ejection, machining allowances and inspection plan with the production objective. Contact Moldiecasting with your part model, alloy preference, volume and quality requirements.
Frequently asked questions
Is Zamak the same as zinc?
No. Zamak is a family of engineered zinc-based alloys with controlled additions of aluminum, magnesium and, in some grades, copper. The alloy designation matters because the grades serve different property and processing needs.
Which Zamak grade is most common?
Zamak 3 is a widely used general-purpose grade because it offers a balanced combination of castability, dimensional stability and finishing performance. The right grade still depends on the part requirement.
Can Zamak be machined after die casting?
Yes. Secondary drilling, tapping and machining may be used for critical features, although an efficient design aims to create as many noncritical features as possible in the die-cast shape.
Is Zamak suitable for outdoor use?
It can be, but suitability depends on the specific environment, finish, coating system, water exposure, galvanic contact and required service life. Validate with the actual corrosion requirement.