

Magnesium and aluminum are both capable die-casting material families, but neither is automatically “better.” The correct choice depends on the part’s weight target, stiffness requirement, operating environment, finishing route, volume, geometry, and the production system that will make it. For B2B sourcing teams, the decision should be made at program level, not from material price or density alone.
This guide compares the two families for high-pressure die casting (HPDC), identifies the design changes a material switch may require, and outlines the inputs needed for a productive tooling review.
Choose the Material by the Part Function
Start with the load case and the commercial objective. A lightweight electronics frame, a pressure-tight automotive housing, a heat-dissipating enclosure, and a cosmetic cover can lead to different material choices even when their CAD geometry appears similar.
| If the priority is | Start the assessment with | Key validation question |
|---|---|---|
| Lowest feasible mass | Magnesium | Can ribs, section modulus, coating, and joining details meet the full service requirement? |
| Stiffness, thermal performance, and broad supply options | Aluminum | Does the selected die-casting alloy meet strength, thermal, and corrosion needs without excessive machining? |
| High-volume repeatability | Either, after DFM | Are gates, vents, thermal control, and machine capability matched to the alloy and geometry? |
| Cost reduction | Total landed cost comparison | Have scrap, finishing, machining, logistics, yield, and expected tooling life been included? |
Magnesium Die Casting: Where It Fits
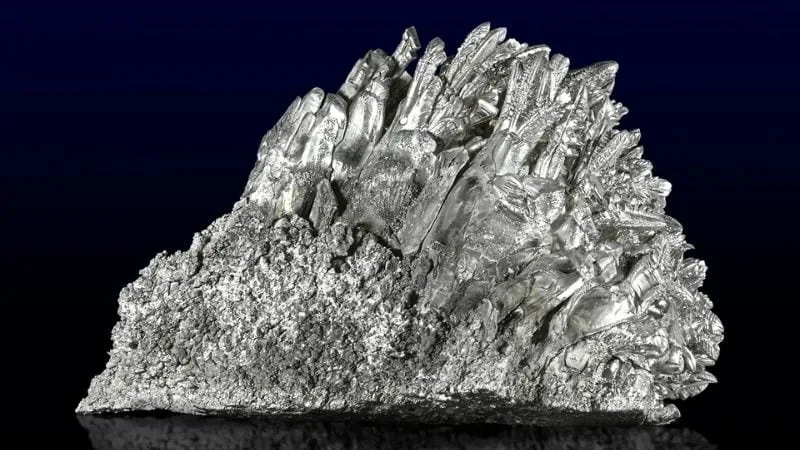
Magnesium alloys have lower density than aluminum alloys and are often selected when every gram matters. Their low density can reduce component mass significantly, but magnesium also has a lower elastic modulus. A direct one-for-one material substitution can therefore create an under-stiff component unless the geometry is redesigned with ribs, section changes, or load-path improvements. For OEM programs that need magnesium tooling, review magnesium molds alongside alloy and DFM constraints early.
Common reasons to evaluate magnesium
- Weight-sensitive structural or semi-structural parts where redesigned geometry can preserve stiffness.
- Electronic housings and frames that benefit from low mass, cast-in detail, and electromagnetic shielding considerations.
- Parts where machining, vibration damping, or integration of multiple features can improve the program-level outcome.
Key engineering cautions
- Evaluate stiffness at component level; specific strength is not a substitute for checking deflection and natural frequency.
- Plan corrosion protection and galvanic isolation where magnesium contacts more noble metals or operates in demanding wet or salt-containing environments.
- Confirm the alloy, melt handling, machine type, safety controls, finishing route, and local production capability before locking the design.
Aluminum Die Casting: Where It Fits
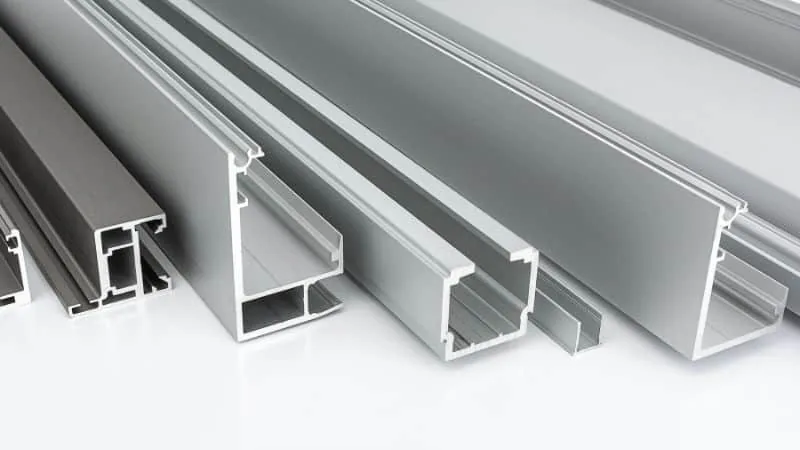
Aluminum die-casting alloys are widely used for housings, covers, brackets, thermal-management parts, and automotive components because they offer a practical balance of stiffness, strength, corrosion behavior, castability, and manufacturing familiarity. Aluminum is often a strong default when structural rigidity, heat flow, and broad process availability are more important than achieving the lowest possible mass. When aluminum is the preferred family, align geometry with aluminium molds and the selected HPDC alloy before steel is cut.
Common reasons to evaluate aluminum
- Rigid housings, covers, and brackets where thermal performance or stable component stiffness is important.
- Applications requiring a mature high-pressure die-casting supply base and a broad choice of alloy and finishing routes.
- Programs where corrosion behavior, cost structure, and recycled-content strategy must be assessed alongside mechanical performance.
Key engineering cautions
- Use properties for the actual die-casting alloy and process condition. Wrought grades such as 6061 should not be treated as a drop-in reference for HPDC alloy performance.
- Control porosity where sealing, welding, plating, pressure containment, or post-machining is critical.
- Model heat flow using the finished geometry, interfaces, and duty cycle rather than relying on a generic conductivity ranking.
Magnesium vs Aluminum: Decision Matrix for Die Cast Parts
The comparison below is directional. Exact outcomes depend on the chosen alloy, wall thickness, tool design, process window, heat treatment or finishing route, and applicable customer specifications.
| Selection factor | Magnesium alloys | Aluminum alloys | What to review in the RFQ |
|---|---|---|---|
| Density / mass | Lower density; potential for meaningful mass reduction. | Higher density, still lightweight for a structural metal. | Mass target, allowable deflection, and geometry freedom. |
| Stiffness | Lower elastic modulus; geometry often needs reinforcement. | Typically higher component stiffness at similar geometry. | FEA load cases, ribs, mounting points, and vibration targets. |
| Strength | Alloy and section dependent; assess at service temperature. | Wide set of HPDC alloy options for strength and rigidity. | Required proof load, fatigue, impact, and temperature range. |
| Thermal role | Application-specific; do not assume a universal advantage. | Often selected for heat-dissipating housings and heat sinks. | Heat sources, interfaces, duty cycle, and allowable temperature rise. |
| Corrosion and joining | Needs deliberate coating and galvanic-corrosion strategy. | Generally favorable natural oxide behavior; system still matters. | Environment, fasteners, coatings, sealing, and repair route. |
| Die-casting process | May use hot- or cold-chamber systems depending on alloy and equipment. | HPDC aluminum is commonly cold-chamber. | Machine availability, melt practice, cycle target, and safety plan. |
| Cost | Assess total program cost, not raw material alone. | Often benefits from broad material and production availability. | Tooling, yield, finishing, machining, logistics, and annual volume. |
Why a Direct Material Swap Usually Fails
Replacing an aluminum casting with magnesium is not simply a density calculation. The stiffness target may change the rib network, wall transitions, bosses, fastener design, draft, ejection layout, and local die temperature strategy. Replacing magnesium with aluminum also requires a new review of fill behavior, part mass, clamping, thermal balance, and machining allowance. Treat either change as a DFM event and validate it before cutting steel.
| Design topic | When switching to magnesium | When switching to aluminum |
|---|---|---|
| Ribs and sections | Use geometry to recover stiffness and manage local stress. | Avoid unnecessary mass; maintain fill-friendly, balanced transitions. |
| Corrosion system | Specify coatings and isolate dissimilar-metal interfaces. | Review finish and isolation for the full assembly environment. |
| Tooling and thermal control | Confirm alloy-specific die, gate, vent, and temperature strategy. | Plan robust cooling and gating for the selected aluminum alloy and part function. |
| Validation | Check deflection, vibration, corrosion, and joining. | Check thermal performance, porosity risk, sealing, and machining response. |
Tooling and Manufacturing Considerations
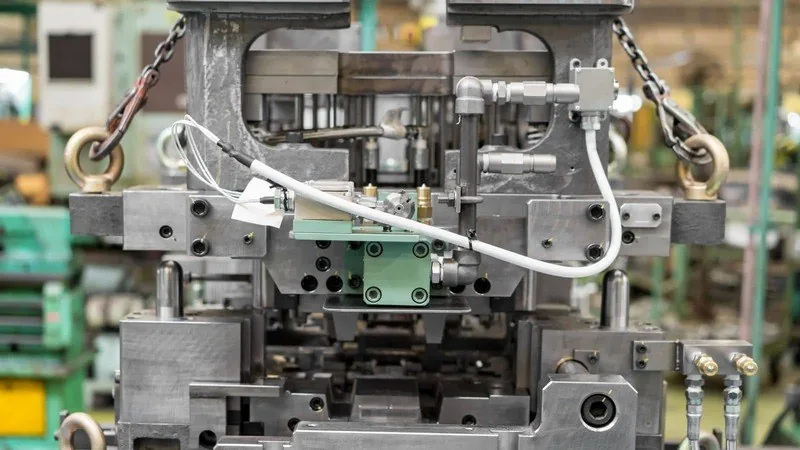
Material selection and tooling design must be developed together. Gate locations, runners, overflows, venting, vacuum provisions, cooling circuits, die steel selection, surface treatment, and ejection all influence yield, dimensional stability, and cosmetic quality. Moldie supports this early-stage review through mold design and engineering, where part geometry and production requirements are translated into a manufacturing-ready tooling concept.
Questions to resolve before tooling release
- Which alloy grade, mechanical-property condition, corrosion exposure, and temperature range apply to the finished part?
- Which surfaces will be machined, sealed, coated, welded, or used for grounding and electrical contact?
- Which dimensions and zones are critical to function, and how will they be inspected?
- What annual volume, cavity strategy, cycle target, and qualification plan are expected?
- Which test evidence is needed: dimensional report, leak test, X-ray/CT, salt-spray exposure, vibration, or assembly validation?
Frequently Asked Questions
Is magnesium always lighter in the finished component?
Magnesium has lower density, but the finished-part saving depends on the geometry required to meet stiffness, fastening, impact, and durability targets. Use component-level analysis rather than comparing equal wall thicknesses only.
Is aluminum always the lower-cost option?
Not necessarily. Aluminum often benefits from availability and established production infrastructure, but a valid comparison includes material yield, machining, coating, cycle time, tool maintenance, logistics, and the value of any weight reduction.
Can the same die be used for both materials?
A material change should not be assumed to be tool-compatible. Alloy behavior, thermal demand, gating, venting, ejection, corrosion needs, and part geometry require a tooling and DFM review before reuse or modification is approved.
Which material is better for an electronics enclosure?
The answer depends on mass, stiffness, heat dissipation, shielding, corrosion, finish, drop performance, and assembly requirements. A design review with the full operating and manufacturing context is more reliable than a generic material preference.
Start Your Magnesium or Aluminum Tooling Review With Moldiecasting
Moldiecasting helps OEM teams evaluate alloy choice alongside geometry, DFM, gate and vent concepts, thermal control, and production requirements. Send your 2D or 3D drawing, target alloy, expected annual volume, critical functional zones, and existing validation data so the project can be reviewed on an engineering and sourcing basis.
Contact Moldiecasting to discuss your magnesium or aluminum die-casting mold program.