
Choosing between a CNC-machined billet part and a cast part is not a simple strength contest. It is a manufacturing decision that affects alloy choice, geometry, tooling investment, machining time, unit cost, quality controls and the path from prototype to volume production. The best route depends on what the part must do and how many you need to make.
For many OEM programs, the practical question is: should we keep machining material away from solid stock, or redesign the component as a near-net-shape casting and invest in production tooling? This guide explains the trade-offs so you can start that discussion with clearer requirements.
First, clarify what billet and cast actually mean
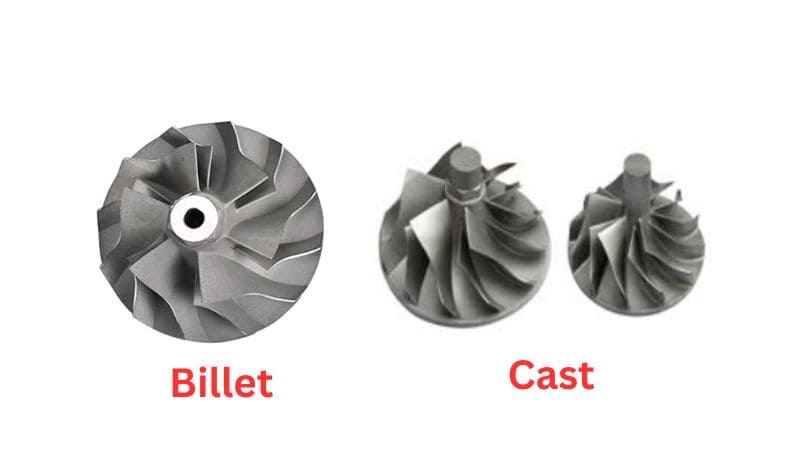
In manufacturing, billet usually describes a semi-finished solid metal form such as bar, block, plate or an extrusion. In everyday engineering conversation, “billet part” commonly means a finished component CNC-machined from that solid stock. The starting material is usually a wrought alloy selected for machinability and specified mechanical properties.
A cast part is formed by filling a mold cavity with molten alloy and allowing it to solidify. Casting is a family of processes, not one process: sand casting, gravity/permanent-mold casting and high-pressure die casting have different capabilities. For high-volume nonferrous parts with detailed geometry, pressure die casting is often the relevant comparison because a reusable steel die produces parts close to final shape.
The distinction matters because billet, cast and forged are not interchangeable alloy grades. A fair comparison begins with the actual alloy, condition, part geometry, required properties and manufacturing process—not with a marketing label.
Billet machining vs casting at a glance
| Decision factor | Billet-machined part | Cast or die-cast part |
|---|---|---|
| Starting point | Wrought bar, block, plate or extrusion | Molten casting alloy and a mold or die |
| How the shape is made | CNC removes material to leave the final shape | The mold creates a near-net shape; critical features may be machined |
| Best fit | Prototypes, lower volumes, frequent design changes, tight machined features | Repeat production, complex geometry, integrated features and lower cost at scale |
| Upfront investment | Programming, fixtures and cutting tools; generally lower dedicated tooling cost | Dedicated mold or die, design and tryout; higher initial investment |
| Per-part economics | Machining time and material removal remain in every unit | Tooling is amortized; cycle time and near-net shape can reduce repeat cost |
| Geometry | Excellent for accessible precision features; deep cavities can add time and tool limitations | Excellent for ribs, bosses, thin-wall features and complex forms when designed for casting |
| Material use | Can generate significant recyclable chips from a large starting block | Near-net shape can reduce removed material, though runners and process scrap remain |
| Quality focus | Material certification, toolpath control, workholding and inspection | Alloy/process control, die design, gating, venting, thermal balance, trimming and inspection |
Where billet machining has an advantage
Machining from solid stock is often the efficient choice during development. You can adjust CAD, update a program and make another part without changing a production die. It is also useful when annual demand is limited, when the design is still moving, or when a feature needs a fine machined finish and is difficult to cast directly.
A billet route can offer predictable material behavior when the specified wrought alloy and temper are appropriate for the load case. However, “machined from billet” is not an automatic guarantee of a stronger component. A part’s real performance still depends on alloy selection, cross-sections, fillets, stress concentrations, surface condition, fastener interfaces and the validation plan.
Where casting and die casting have an advantage
Casting becomes compelling when the component needs geometry that would take extensive machining to create: integrated ribs, bosses, housings, pockets, draftable internal features or repeated complex contours. A well-designed casting can place material where it supports the function and avoid paying to remove it from a larger solid block.
For repeat production, high-pressure die casting can provide rapid, consistent cycles once the die is proven. The economic benefit comes from spreading the tooling investment over many parts and minimizing secondary operations—not from assuming that every cast feature requires no finishing. Threads, precision bores, sealing faces and critical datums may still need CNC machining after casting.
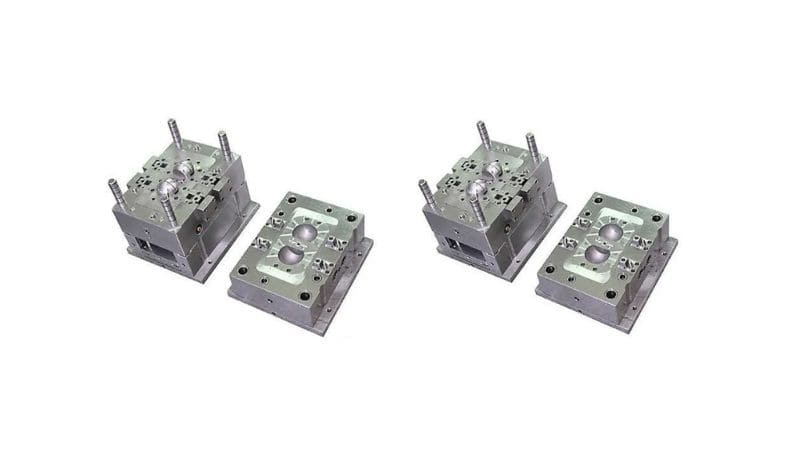
If your program is moving toward repeat aluminum production, explore Moldiecasting aluminum die casting molds. The team can review whether your component is suited to die-cast geometry before tooling is released.
Material properties: compare specifications, not assumptions
Wrought and cast aluminum alloys are developed for different routes. Wrought grades are commonly processed by rolling, extrusion and machining; casting alloys are formulated for fluidity, filling behavior and solidification performance. That means a 6061-T6 billet part and an A380 die casting should not be evaluated by one strength number alone.
For a meaningful comparison, request the property values that match the application: yield strength, tensile strength, elongation, hardness, fatigue needs, corrosion environment, thermal behavior and any certification requirements. Then compare those values in the relevant product form and section thickness. Discuss whether pressure tightness, weldability, heat treatment or surface finishing changes the alloy or process choice.
Casting quality also depends on design and process discipline. Proper gating, venting, overflow, cooling, alloy handling and process monitoring are central to managing risks such as porosity, shrinkage and inclusions. Conversely, machining cannot rescue a design that starts with excessive stress concentration or insufficient section strength.
Cost: use total program cost, not only piece price
Billet machining usually starts with a lower commitment because it avoids a dedicated production die. But each part carries machining cycle time, tool wear, setup and material-removal cost. It can remain the right choice for prototypes, service parts and modest volumes, especially where geometry is simple or likely to change.
Casting adds an upfront tooling phase: DFM review, mold design, steel selection, manufacturing, tryout and any revisions needed to achieve a stable process. Once volume rises and the design is frozen, near-net-shape production may reduce the material removed and the time spent machining every unit. The break-even point is specific to the part, target quality, number of cavities, finish requirements and expected lifetime volume.
A useful quotation package includes a 3D model and drawing, annual and lifetime quantities, target alloy, tolerances, critical-to-function features, cosmetic expectations, leak or pressure requirements, secondary operations, inspection plan and desired launch date. This lets suppliers compare routes on a realistic basis.
Design rules that make a casting program more successful
A component designed only for billet machining may need changes before it can be cast efficiently. Early DFM can identify where to add draft, maintain more uniform wall thickness, place ribs, provide radii, define parting lines, avoid isolated heavy sections and reserve machining allowance only where it adds functional value. These changes help the metal fill and solidify predictably and make ejection and finishing more reliable.
The best time to discuss these decisions is before steel is cut. Moldie designs and manufactures production tooling with DFM support for gating, cooling and manufacturability. For an application-specific review, see the die casting mold design and manufacturing service and send the part model with your production requirements.
Aluminum, zinc or magnesium: choose the route and the material together
Aluminum is a common choice when a part needs a useful balance of weight, stiffness, heat performance and corrosion resistance. Zinc die casting can be attractive for detailed, thin-wall or hardware-type components, while magnesium may be considered where mass reduction is a leading requirement. The correct material choice depends on function, environment, size, mechanical requirements, finishing and the production process.
Moldiecasting also builds zinc die casting molds and magnesium die casting molds. Discussing the alloy family early helps align die design, thermal management and the casting process with the product requirement.
A practical decision checklist
Choose billet machining first when: the design is evolving; volume is limited; a fast prototype is needed; or the part is dominated by accessible precision-machined features.
Evaluate casting first when: demand is repeatable; the part has complex, draftable geometry; integrated features can replace assemblies; or machining waste and cycle time are becoming costly.
Keep secondary machining in the plan when: the design has threads, tight bores, sealing faces, bearing seats or inspection-critical datums.
Ask for a DFM review before committing when: wall thickness varies widely, the part needs internal features, the cosmetic standard is demanding, or quality risks could affect launch timing.
Ready to evaluate your part?
The right answer is often a staged plan: machine early samples from billet, use the learning to refine the design, then move to a production casting once the geometry and demand justify tooling. A focused DFM review can identify the risks, preserve critical features and clarify the likely cost drivers before you commit.
Request a die casting mold review and quote: Contact Moldiecasting with your 3D model, drawing, alloy preference, annual quantity and critical requirements.
Frequently asked questions
Is billet aluminum always stronger than cast aluminum?
Not automatically. Wrought stock often offers a different property profile from a cast alloy, but engineering performance must be assessed using the specified alloy, condition, section thickness, geometry and load case. A correctly designed casting can be the best solution for its intended function.
Does die casting eliminate machining?
No. Die casting can create many features close to final shape, but critical bores, threads, sealing faces and tight datums frequently receive secondary machining.
When does die casting become more economical than billet machining?
There is no universal quantity threshold. Compare the tooling investment and development time with the recurring machining, material-removal and assembly costs across the expected production volume.
Can the same design be machined first and die cast later?
Often, but the design should receive a dedicated DFM review before tooling. Draft, wall thickness, radii, ribs, parting lines and machining allowances may need to change for robust casting production.